Metric Tap Drill Chart (M2 to M30)
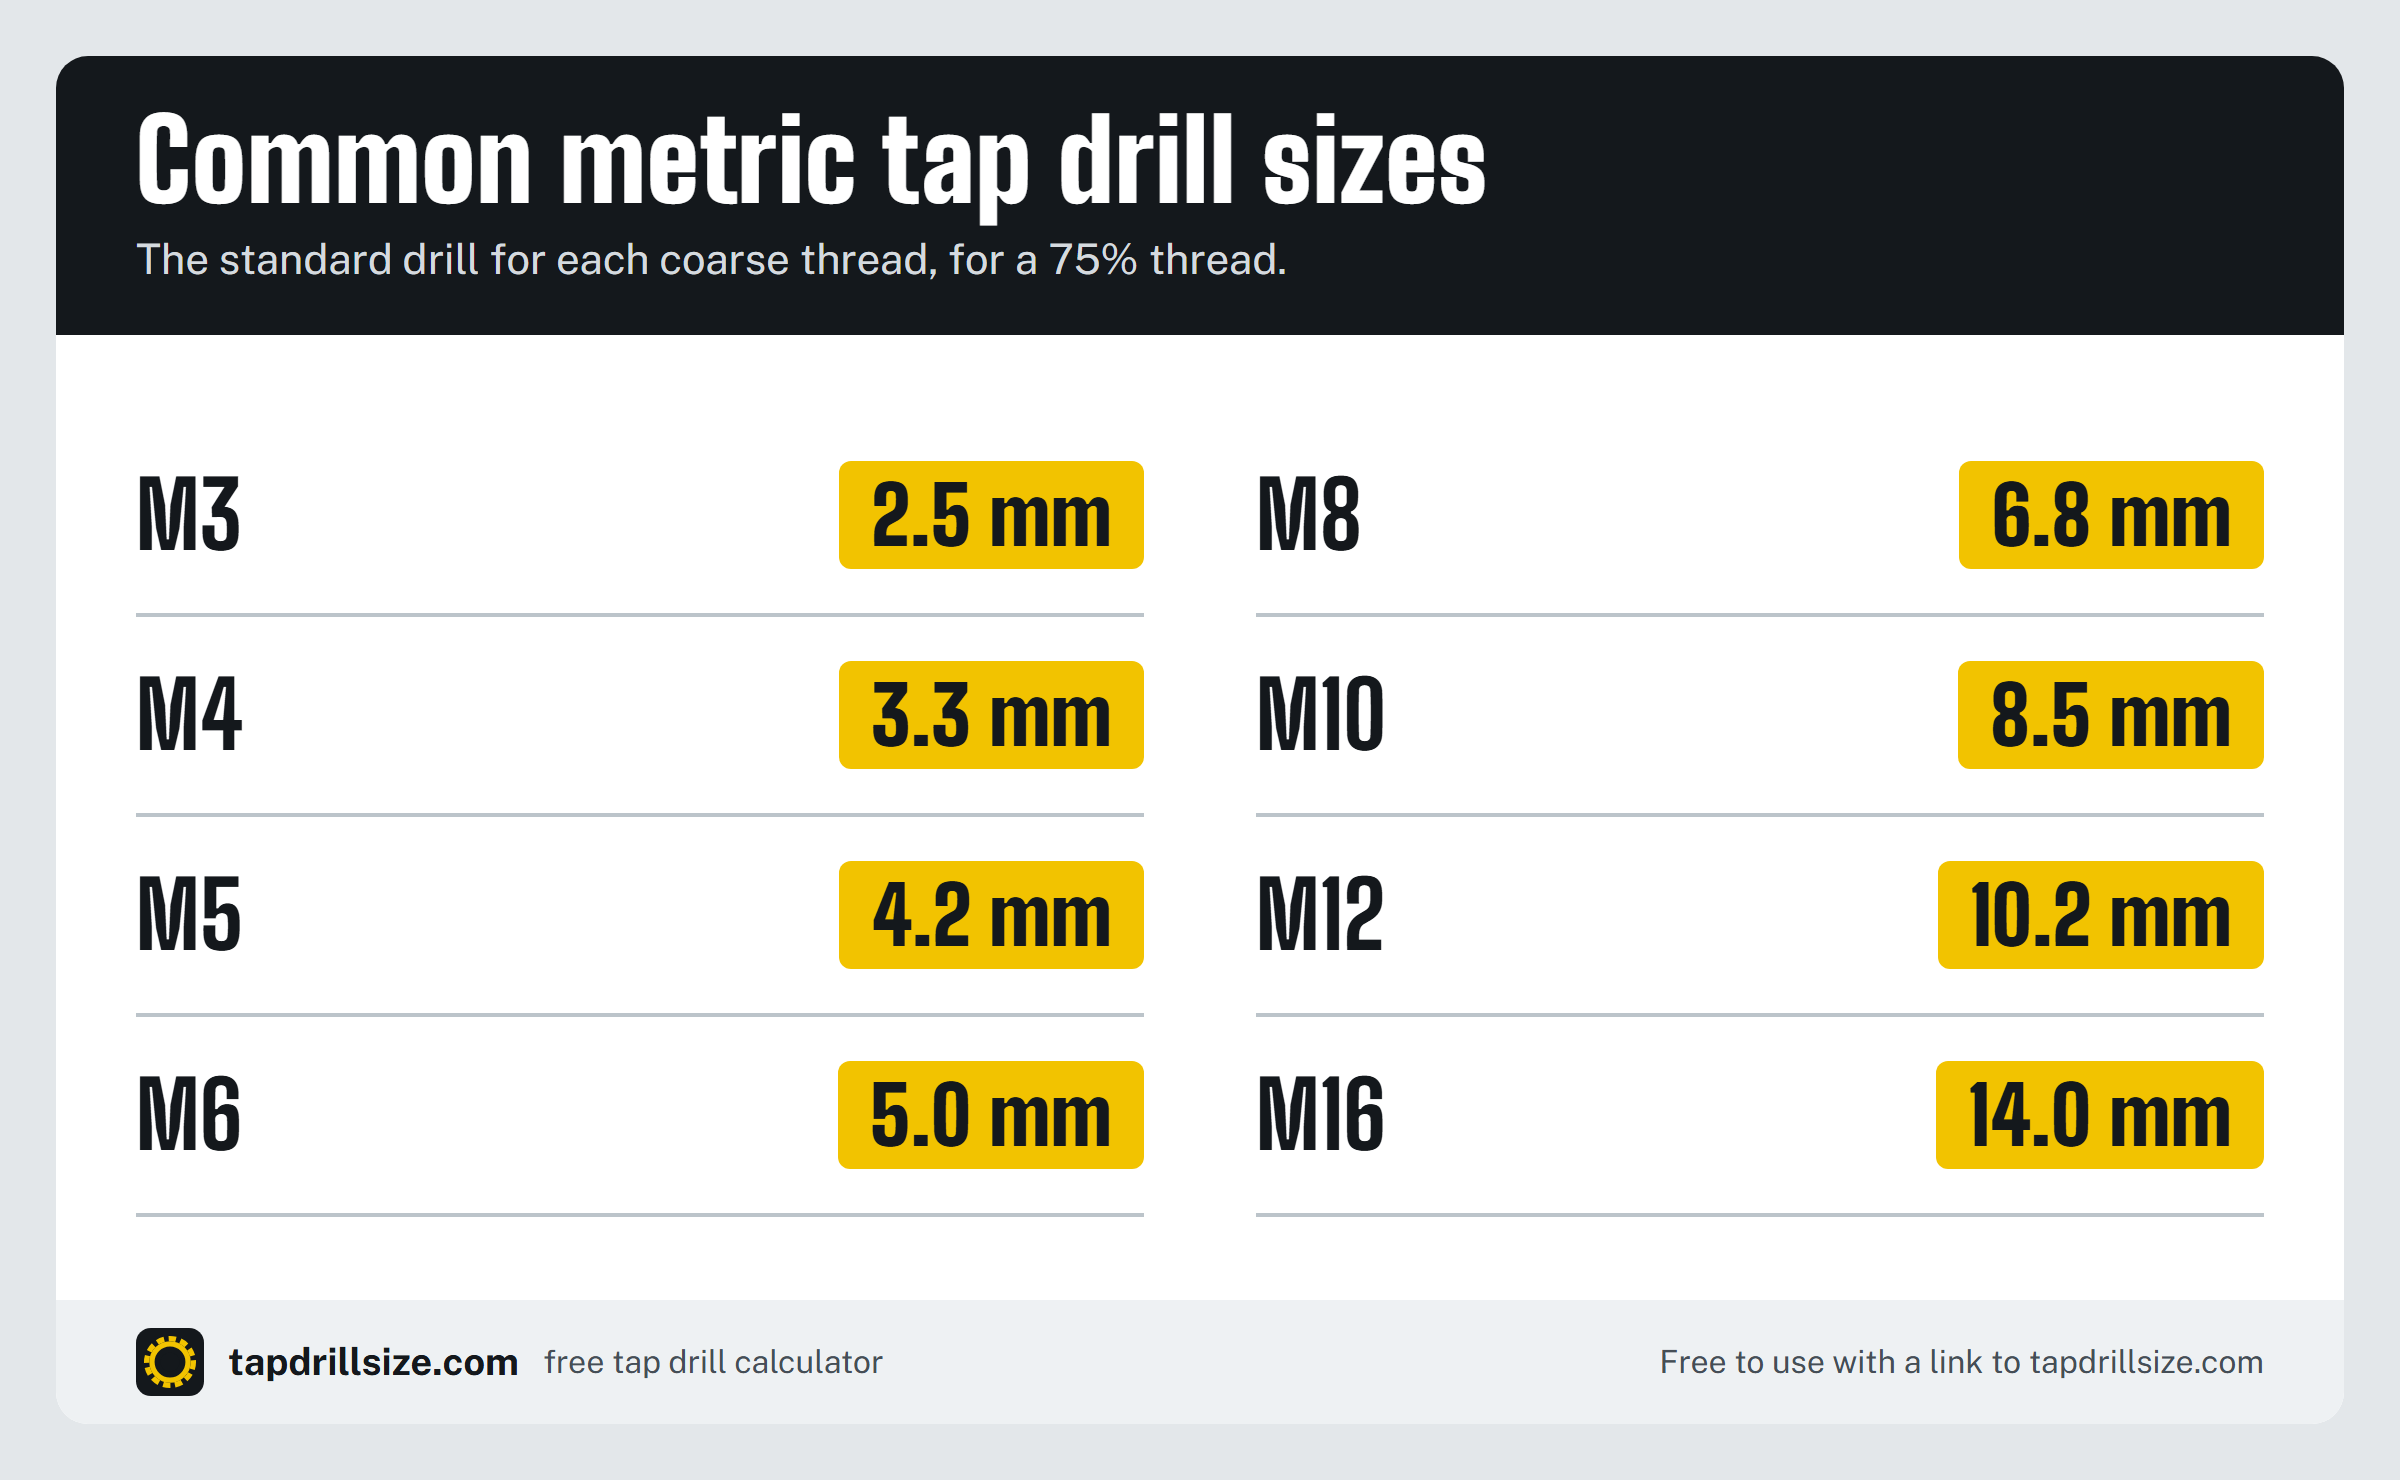
For metric coarse threads, the tap drill is the nominal size minus the pitch: M6 x 1.0 takes 5.0 mm, M8 x 1.25 takes 6.8 mm. Fine pitches such as M8 x 1 and M30 x 2 are in the second table below.
| Thread | Series | Major diameter | Pitch | Aluminum, brass (75%) | Mild steel (60%) | Stainless, titanium (50%) |
|---|---|---|---|---|---|---|
| M2 | Metric coarse | 2.000 mm (0.0787 in) | 0.40 mm | 1.6 mm 77% | 1.7 mm 58%, over 6H | 1.7 mm 58%, over 6H |
| M2.5 | Metric coarse | 2.500 mm (0.0984 in) | 0.45 mm | 2.05 mm 77% | 2.1 mm 68% | 2.2 mm 51%, over 6H |
| M3 | Metric coarse | 3.000 mm (0.1181 in) | 0.50 mm | 2.5 mm 77% | 2.6 mm 62%, over 6H | 2.7 mm 46%, over 6H |
| M3.5 | Metric coarse | 3.500 mm (0.1378 in) | 0.60 mm | 2.9 mm 77% | 3.0 mm 64% | 3.1 mm 51%, over 6H |
| M4 | Metric coarse | 4.000 mm (0.1575 in) | 0.70 mm | 3.3 mm 77% | 3.4 mm 66% | 3.5 mm 55%, over 6H |
| M5 | Metric coarse | 5.000 mm (0.1969 in) | 0.80 mm | 4.2 mm 77% | 4.4 mm 58%, over 6H | 4.5 mm 48%, over 6H |
| M6 | Metric coarse | 6.000 mm (0.2362 in) | 1.00 mm | 5.0 mm 77% | 5.2 mm 62%, over 6H | 5.3 mm 54%, over 6H |
| M8 | Metric coarse | 8.000 mm (0.3150 in) | 1.25 mm | 6.8 mm 74% | 7.0 mm 62%, over 6H | 7.2 mm 49%, over 6H |
| M10 | Metric coarse | 10.000 mm (0.3937 in) | 1.50 mm | 8.5 mm 77% | 8.8 mm 62%, over 6H | 9.0 mm 51%, over 6H |
| M12 | Metric coarse | 12.000 mm (0.4724 in) | 1.75 mm | 10.2 mm 79% | 10.6 mm 62%, over 6H | 10.9 mm 48%, over 6H |
| M14 | Metric coarse | 14.000 mm (0.5512 in) | 2.00 mm | 12.0 mm 77% | 12.4 mm 62%, over 6H | 12.7 mm 50%, over 6H |
| M16 | Metric coarse | 16.000 mm (0.6299 in) | 2.00 mm | 14.0 mm 77% | 14.4 mm 62%, over 6H | 14.7 mm 50%, over 6H |
| M18 | Metric coarse | 18.000 mm (0.7087 in) | 2.50 mm | 15.5 mm 77% | 16.1 mm 59%, over 6H | 16.4 mm 49%, over 6H |
| M20 | Metric coarse | 20.000 mm (0.7874 in) | 2.50 mm | 17.5 mm 77% | 18.1 mm 59%, over 6H | 18.4 mm 49%, over 6H |
| M22 | Metric coarse | 22.000 mm (0.8661 in) | 2.50 mm | 19.5 mm 77% | 20.1 mm 59%, over 6H | 20.4 mm 49%, over 6H |
| M24 | Metric coarse | 24.000 mm (0.9449 in) | 3.00 mm | 21.0 mm 77% | 21.7 mm 59%, over 6H | 22.1 mm 49%, over 6H |
| M30 | Metric coarse | 30.000 mm (1.1811 in) | 3.50 mm | 26.5 mm 77% | 27.3 mm 59%, over 6H | 27.8 mm 48%, over 6H |
Small percentages show the thread engagement each drill leaves. "Over 2B" (6H for metric) marks a hole bigger than the maximum minor diameter of the usual thread class, and "under" one smaller than the minimum. Such a drill is out of tolerance for that class, so check the class on your drawing first. Click a thread for its full page, which names a drill inside the limits.
Metric Tap Drill Chart (M2 to M30) | tapdrillsize.com/metric-tap-drill-chart/ | Last reviewed October 12, 2026 | Check your tap maker's chart before cutting.
How to read a metric thread name
M6 x 1.0 means a 6 mm major diameter and a 1.0 mm pitch, the distance from one thread to the next. A thread written as plain M6 has the coarse pitch, the default for that diameter (Wikipedia). This chart lists the coarse pitches.
Why major minus pitch
Subtracting the pitch from the major diameter leaves about 77% of a full thread at every size. A full thread needs a hole of the major diameter minus 1.299 times the pitch, and 1 divided by 1.299 is 0.77.
Fine-pitch metric tap drills
A fine thread has a smaller pitch at the same diameter, so it needs a drill closer to the major diameter. The pitches below come from the ISO table on Wikipedia.
| Thread | Pitch | Drill | Size | Thread left | Coarse thread of that size |
|---|---|---|---|---|---|
| M4 x 0.5 | 0.5 mm | 3.5 mm | 0.1378 in | 77% | M4 x 0.7: 3.3 mm |
| M5 x 0.5 | 0.5 mm | 4.5 mm | 0.1772 in | 77% | M5 x 0.8: 4.2 mm |
| M6 x 0.75 | 0.75 mm | 5.3 mm | 0.2087 in | 72% | M6 x 1.0: 5.0 mm |
| M8 x 1 | 1 mm | 7.0 mm | 0.2756 in | 77% | M8 x 1.25: 6.8 mm |
| M10 x 1.25 | 1.25 mm | 8.8 mm | 0.3465 in | 74% | M10 x 1.5: 8.5 mm |
| M10 x 1 | 1 mm | 9.0 mm | 0.3543 in | 77% | M10 x 1.5: 8.5 mm |
| M12 x 1.5 | 1.5 mm | 10.5 mm | 0.4134 in | 77% | M12 x 1.75: 10.2 mm |
| M12 x 1.25 | 1.25 mm | 10.8 mm | 0.4252 in | 74% | M12 x 1.75: 10.2 mm |
| M14 x 1.5 | 1.5 mm | 12.5 mm | 0.4921 in | 77% | M14 x 2.0: 12.0 mm |
| M16 x 1.5 | 1.5 mm | 14.5 mm | 0.5709 in | 77% | M16 x 2.0: 14.0 mm |
| M18 x 1.5 | 1.5 mm | 16.5 mm | 0.6496 in | 77% | M18 x 2.5: 15.5 mm |
| M20 x 1.5 | 1.5 mm | 18.5 mm | 0.7283 in | 77% | M20 x 2.5: 17.5 mm |
| M20 x 2 | 2 mm | 18.0 mm | 0.7087 in | 77% | M20 x 2.5: 17.5 mm |
| M22 x 1.5 | 1.5 mm | 20.5 mm | 0.8071 in | 77% | M22 x 2.5: 19.5 mm |
| M24 x 2 | 2 mm | 22.0 mm | 0.8661 in | 77% | M24 x 3.0: 21.0 mm |
| M30 x 2 | 2 mm | 28.0 mm | 1.1024 in | 77% | M30 x 3.5: 26.5 mm |
We found no published chart for these fine sizes. Each drill is the major diameter minus the pitch, rounded to the nearest 0.1 mm with ties going to the larger drill, and the percentage uses the same formula as every other row.
Metric sizes and their inch lookalikes
Some metric sizes sit very close to an inch size. They have different pitches and are not interchangeable.
| Metric | Closest inch size | Diameter difference | Metric pitch | Inch pitch |
|---|---|---|---|---|
| M2 | #2-56 | 0.18 mm | 0.4 mm | 0.454 mm |
| M2.5 | #2-56 | 0.32 mm | 0.45 mm | 0.454 mm |
| M3 | #4-40 | 0.16 mm | 0.5 mm | 0.635 mm |
| M3.5 | #6-32 | 0.01 mm | 0.6 mm | 0.794 mm |
| M4 | #8-32 | 0.17 mm | 0.7 mm | 0.794 mm |
| M5 | #10-24 | 0.17 mm | 0.8 mm | 1.058 mm |
| M6 | 1/4-20 | 0.35 mm | 1.0 mm | 1.27 mm |
| M8 | 5/16-18 | 0.06 mm | 1.25 mm | 1.411 mm |
| M10 | 3/8-16 | 0.48 mm | 1.5 mm | 1.587 mm |
| M14 | 9/16-12 | 0.29 mm | 2.0 mm | 2.117 mm |
| M16 | 5/8-11 | 0.13 mm | 2.0 mm | 2.309 mm |
| M22 | 7/8-9 | 0.22 mm | 2.5 mm | 2.822 mm |
FAQ
What is the tap drill size for M6?
5.0 mm (0.1969 in) leaves about 77% thread. M6 x 1.0 is the coarse pitch, so the drill is the 6 mm major diameter minus the 1.0 mm pitch.
What is the tap drill size for M8 x 1?
7.0 mm leaves about 77% thread. That is the fine pitch, so the drill is bigger than the 6.8 mm used for the coarse M8 x 1.25.
What is the tap drill size for M10 x 1.25?
8.8 mm leaves about 74% thread. M10 x 1.25 is a fine pitch of M10, which is coarse at 1.5 mm and takes 8.5 mm.
What is the tap drill size for M30 x 2?
28.0 mm leaves about 77% thread. The coarse M30 x 3.5 takes 26.5 mm, so check the pitch before you drill.
Why is the metric tap drill the thread size minus the pitch?
It leaves about 77% of a full thread at every size, close to the 75% most charts aim for. A full thread needs a hole of the major diameter minus 1.299 times the pitch, and 1 divided by 1.299 is 0.77. Wikipedia gives the same rule of thumb.
Chart drills are major minus pitch, checked against the Fabworks tap drill chart. Thread percentages use the formula printed in the OSG tap drill chart, Vol 3 (2024). Pitches from Wikipedia: ISO metric screw thread. Last reviewed October 12, 2026. Method: how the numbers are calculated.